 EN

What Standards Should a Colored Tissue Paper Manufacturer Follow for Safety?
For a colored tissue paper manufacturer, safety is not a single certificate or a reassuring phrase on a quotation. It is a repeatable way of controlling the fibers, dyes, additives, converting process, and records behind each order. From a packaging-paper technical advisor’s perspective, the starting point is the intended use: gift wrapping, box lining, decorative packing, or direct food contact all create different questions.
That distinction matters because colored tissue paper can look similar across applications while carrying very different compliance expectations. A buyer should ask for evidence tied to the actual market, contact conditions, color system, and finished format. This article sets out a practical safety-control framework a colored tissue paper manufacturer can use and a procurement team can review.
1. Start with the intended use, not a generic “safe” claim
The first specification should state what the colored tissue paper will touch, how long contact lasts, whether it may become wet or greasy, and where it will be sold. Tissue used as an outer presentation layer for dry boxed gifts does not face the same review as material intended to contact food directly. If the paper is mainly used for presentation rather than protection, that distinction should be visible in the product description and sales documents.
For food-contact applications, a colored tissue paper manufacturer should map the construction and conditions of use before selecting compliance evidence. In the United States, 21 CFR 176.170 addresses paper and paperboard components that contact aqueous and fatty foods, with listed substances and conditions of use. It is a useful regulatory reference, but it is not a blanket approval for every colored tissue paper. The finished product, colorants, processing aids, and intended contact conditions still need to be checked together.
For non-food packaging, the review may focus more heavily on chemical restrictions, color transfer, odor, storage, and end-use claims. Plain-language clarification helps here: “suitable for gift-box lining” is a bounded application statement; “safe for all uses” is not.
2. Control raw materials with a documented material list
A reliable colored tissue paper manufacturer should keep a current bill of materials for each grade. This list should identify the fiber source, dyes or pigments, wet-strength agents if used, retention aids, coatings, and any converting materials that can affect the final sheet. Each supplier change should trigger a review rather than being treated as an invisible purchasing substitution.
- Fiber and base sheet: define grade, cleanliness requirements, and whether recycled content is permitted for the intended use.
- Color system: record the dye or pigment identity, supplier documentation, shade target, and any restrictions for the destination market.
- Process chemicals: identify functional additives and retain their technical and safety documentation.
- Packaging and converting inputs: include inks, adhesives, cores, and wraps when they can create contact or odor concerns.
REACH is an EU framework designed to improve protection from chemical risks. For orders going to Europe, the practical question is not whether a supplier can simply say “REACH compliant.” It is whether the relevant restricted substances, intended article, and up-to-date supplier declarations have been reviewed for that order. A colored tissue paper manufacturer should keep declarations versioned and traceable to the materials actually used.
3. Verify color fastness and migration risk on the finished paper
Color is a functional feature, but it can also create a transfer risk. A beautiful sample is not the finished workflow: tissue may be folded, rubbed against a product, exposed to humidity, or packed under pressure. The correct test plan depends on the use case, so a manufacturer should agree it with the buyer or an appropriate laboratory before claiming performance.
EN 646 is commonly referenced for evaluating the color fastness of dyed or printed paper and board intended for food contact. A colored tissue paper manufacturer should confirm the current applicable version, sample conditioning, and acceptance criteria with the testing provider. It is better to describe a completed test precisely than to attach an unqualified “food-safe color” label.
| Control point | Why it matters | Evidence to retain |
|---|---|---|
| Shade approval | Prevents ambiguity between a digital image and the approved production color. | Signed or otherwise traceable shade standard and lot reference. |
| Dry and wet rub review | Helps assess whether color may transfer during realistic handling. | Test method, conditioning details, result, and release decision. |
| Food-contact migration review | Addresses the specific contact scenario instead of a generic safety claim. | Applicable regulation, laboratory scope, material list, and report. |
| Odor and cleanliness check | Can affect premium packaging and sensitive contents. | Inspection record and corrective-action log if needed. |
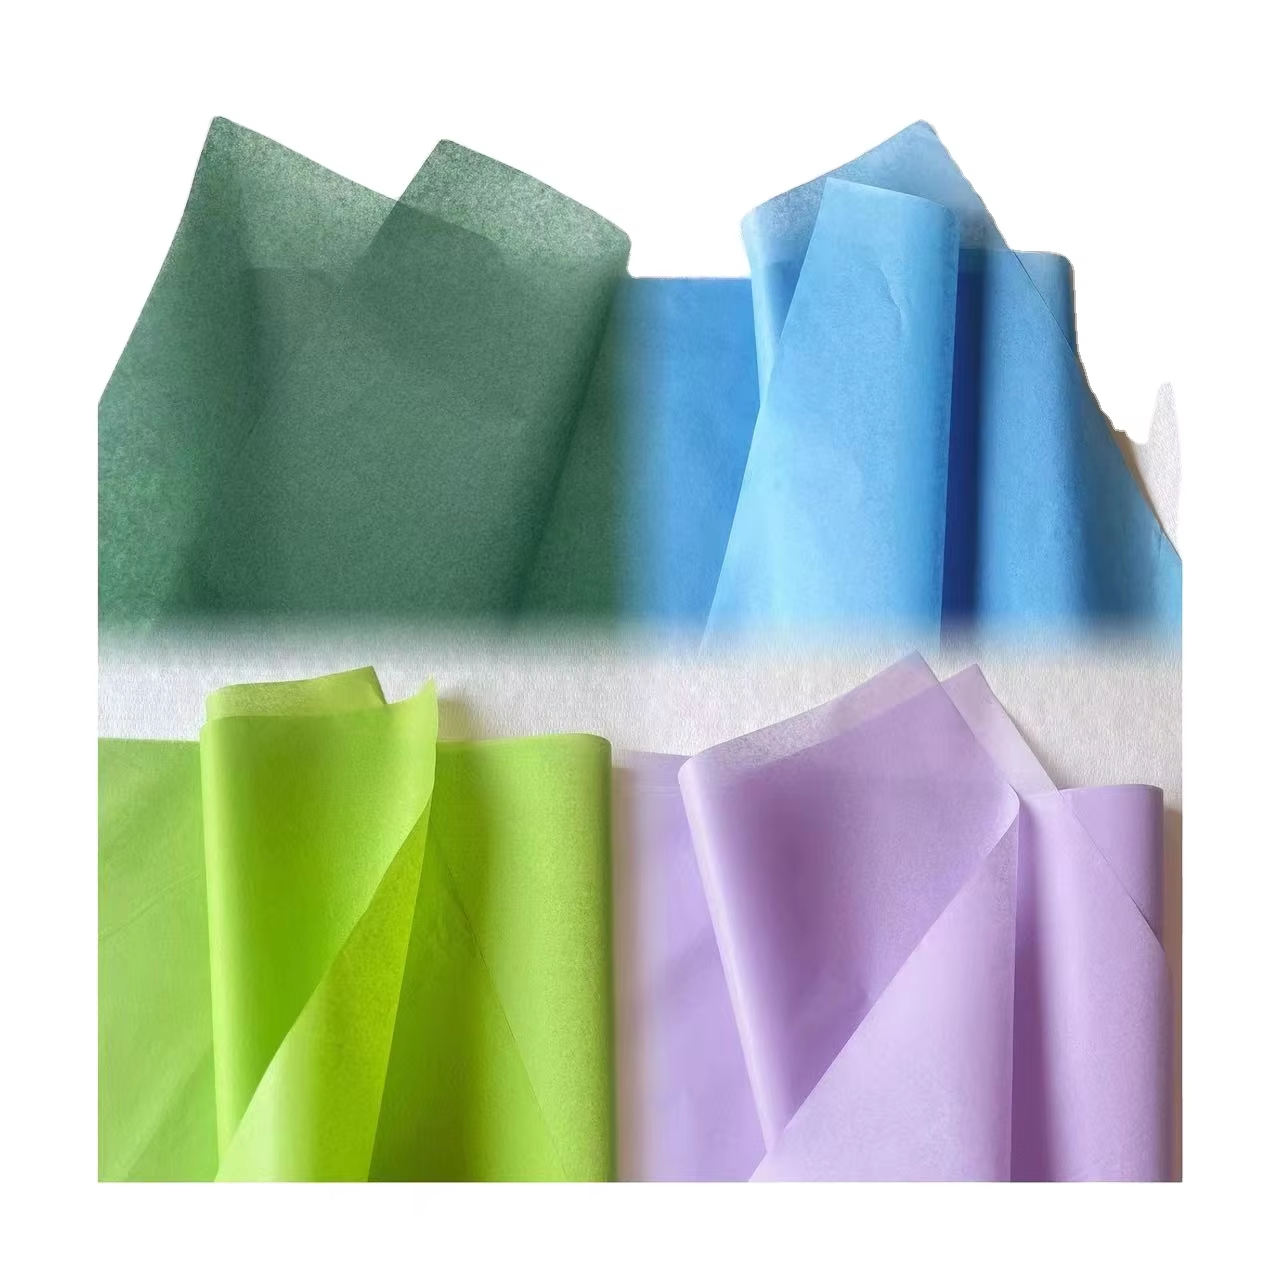 Sample review should connect the approved color to the intended packing and handling conditions.
4. Build traceability from color approval to shipment
Safety control becomes credible when the manufacturer can connect a roll or sheet shipment back to its inputs and production conditions. The relevant question is not only which shade was approved, but how that shade behaves in the packing workflow and which lot produced it.
At a minimum, a colored tissue paper manufacturer should be able to link the customer order, approved specification, raw-material lots, production date, machine or line, quality checks, and shipping lot. This does not require publishing confidential formulas. It requires an internal record structure that can support a targeted investigation if a buyer reports staining, odor, unexpected shade variation, or a documentation request.
For custom colored tissue paper, retain the approved Pantone or physical reference, tolerance instructions, and any notes about one-sided color, sheets versus rolls, or pack-out conditions. The question changes from “what is the price?” to “what format and control points reduce unnecessary handling or approval risk?”
5. Separate certifications, test reports, and supplier declarations
These documents are useful, but they do not mean the same thing. A responsible colored tissue paper manufacturer should label them accurately in its sales file.
- Certification: usually confirms that a system, chain of custody, or defined scope has been assessed. It should be checked for holder, scope, validity, and claimed product coverage.
- Test report: describes a tested sample, method, and result. Confirm that the sample represents the supplied grade and requested color.
- Supplier declaration: provides input-level information and should be current, specific, and backed by controlled material data.
- Specification sheet: translates the agreed grade into measurable order requirements; it should not overstate untested safety outcomes.
Putian C&Q Paper Co., Ltd. identifies white, colored, and food-grade tissue paper within its stated product scope. For any safety-sensitive inquiry, the appropriate next step is to request the current specification, applicable documentation, and sample-review plan for the exact grade rather than assuming that one document covers every color and application.
6. Use a release checklist before each production lot ships
A short release checklist can make a large difference. Before shipment, the colored tissue paper manufacturer should confirm that the purchase order matches the approved application, color reference, sheet or roll format, labeling, and destination-market documentation. Then compare the production record and quality checks with the agreed specification.
- Confirm the intended use and destination market on the order record.
- Verify the approved color reference and production lot identity.
- Check the current material declarations and any required test-report scope.
- Review finished-paper appearance, cleanliness, odor, and relevant color-transfer checks.
- Ensure rolls, sheets, and outer packaging are correctly labeled for traceability.
- Record deviations and obtain a documented disposition before release.
This is not paperwork for its own sake. It gives buyers a clear route from an application claim to the evidence that supports it.
Conclusion: make safety evidence specific to the paper’s use
A capable colored tissue paper manufacturer does more than produce an attractive shade. It defines the intended use, controls the material list, checks color-transfer risk, maintains traceability, and presents certifications and reports within their real scope. For buyers, the most useful RFQ includes the destination, whether direct food contact is intended, the expected handling conditions, color reference, format, and required documents.
Ask for a sample and review it in the actual pack-out sequence. That practical step helps turn colored tissue paper from a visual choice into a documented, application-appropriate packaging decision.